Zylidac Bio LLC is a U.S.-based biologics contract development and manufacturing organisation (CDMO) operating within the Zydus Lifesciences group. The company was established in July 2025 and formally launched its operations following Zydus Lifesciences’ acquisition of Agenus’ biologics manufacturing assets in January 2026. The acquisition included facilities in Emeryville and Berkeley, California, giving Zydus an established U.S. manufacturing presence and entry into the global biologics CDMO market.
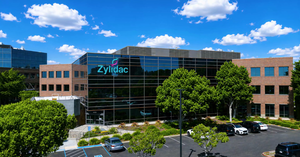
The company’s principal operational asset is an 83,000-square-foot commercial-scale cGMP biologics manufacturing facility in Emeryville, California, designed to support integrated development and manufacturing activities. Unlike conventional CDMOs that distribute process development, drug substance manufacturing, and drug product operations across multiple locations, Zylidac operates an integrated model that brings these services together under one site, one quality management system, and one master services agreement.
Its infrastructure includes single-use bioreactor capacity comprising one 100-litre system, one 500-litre system, and four 2,000-litre systems, alongside automated sterile filling, analytical laboratories, GMP warehousing, labeling, and secondary packaging capabilities. The company reports more than $100 million invested in facility and capital upgrades and a workforce exceeding 90 full-time-equivalent employees.
Zylidac’s technical team brings longstanding experience in complex biologics development, having conducted more than 40 cell banking programmes and advanced over 30 molecules into clinical development. Its development and manufacturing capabilities cover monoclonal antibodies, bispecific and multispecific antibodies, fusion proteins, biosimilars, and other complex recombinant proteins.
The company particularly emphasises continuity between development and manufacturing, seeking to minimise technology transfer requirements, improve process knowledge retention, and reduce the operational risks associated with outsourcing different stages of biologics production to separate service providers.
Key Products and Services
Cell Line Development
-
Manufacturability assessment and evaluation of expression systems for biologics programmes.
-
Cell line screening, clone selection, cloning, stability testing, and development of production cell lines.
-
Cell bank generation and supporting documentation with electronic clone traceability.
-
Expression system flexibility to accommodate different biologic modalities and client-specific manufacturing objectives.
Upstream Process Development
-
Cell culture process development for monoclonal antibodies, bispecific antibodies, fusion proteins, and other complex biologics.
-
Media and feed optimisation to improve productivity, consistency, and manufacturing performance.
-
Clone selection, process characterisation, and development of scalable production processes.
-
Process validation support from Investigational New Drug (IND) applications through Biologics License Application (BLA) submissions.
-
Integration of development equipment and commercial manufacturing systems to simplify scale-up and technology transfer.
Downstream Process Development
-
Purification process development for monoclonal antibodies, bispecific antibodies, fusion proteins, and other recombinant biologics.
-
Adaptation of established purification unit operations to molecule-specific physicochemical characteristics.
-
Production of purified materials for formulation development and preclinical pharmacokinetic studies.
-
Process characterisation, validation protocol development, and evaluation of validation results.
-
Lifecycle support through clinical development and commercial manufacturing.
Formulation Development
-
Development and optimisation of liquid biologic formulations.
-
Evaluation of pH, buffer composition, solubility, and other critical formulation parameters.
-
Amino acid- and sugar-based formulation screening approaches.
-
Formulation robustness assessment and container-closure compatibility evaluation.
-
Generation of formulation data to support regulatory submissions.
Analytical Development and Testing
-
Development and qualification of biochemical, biological, and physicochemical analytical methods.
-
Mass spectrometry-based impurity identification and structural characterisation.
-
Product characterisation, impurity profiling, and particle analysis.
-
Container-closure integrity testing and visual inspection.
-
cGMP microbiology testing covering bioburden, endotoxins, sterility, mycoplasma, and viral contaminants.
-
Analytical support for process development, manufacturing, regulatory filings, and product release activities.
cGMP Drug Substance Manufacturing
-
Clinical and commercial-scale biologics drug substance manufacturing.
-
Single-use bioreactor infrastructure comprising 100 L, 500 L, and four 2,000 L systems.
-
Upstream cell culture manufacturing and downstream purification operations.
-
Manufacturing of monoclonal antibodies, bispecific antibodies, biosimilars, fusion proteins, and other complex biologics.
-
Integrated process documentation, specifications, standard operating procedures, and quality management systems.
-
GMP warehouse infrastructure supporting 2–8°C and −20°C storage.
Drug Product Manufacturing and Sterile Fill-Finish
-
Sterile fill-finish of biologic drug products using automated robotic filling technology.
-
Non-interventional robotic filling designed to minimise human contact with sterile products.
-
Vial filling across sizes ranging from 2 mL to 25 mL.
-
100% visual inspection and Acceptance Quality Limit (AQL) sampling.
-
Integrated drug substance-to-drug product manufacturing within a single facility.
-
Manufacturing support for clinical and commercial biologics programmes.
Secondary Packaging, Labeling and Serialization
-
Automated vial labeling with lot numbers and expiration dates printed inline.
-
Serialization capabilities supporting pharmaceutical traceability requirements.
-
Automated cartoning and secondary packaging.
-
Packaging configurations for clinical and commercial distribution.
-
Custom inserts and commercial branding support.
Technology Transfer and Commercialisation
-
Structured technology transfer assessments for incoming biologics programmes.
-
Gap analysis of process documentation and manufacturing parameters.
-
Risk identification and mitigation planning before process implementation.
-
Process validation, manufacturing readiness, and commercial production support.
-
Integrated project execution designed to minimise transfers between development and manufacturing providers.
Strategic Partnerships and Technology Development
Prolific Machines — Optogenetics-Enabled Biologics Manufacturing
In October 2026, Zylidac Bio announced a partnership with Emeryville-based Prolific Machines to advance the scale-up of optogenetics-enabled biologics manufacturing technology from early development into GMP production.
Prolific Machines’ platform combines engineered cell lines, light-controlled protein expression, artificial intelligence-driven process optimisation, and advanced analytics to provide more precise control over biologics manufacturing. The technology is intended to improve yield, product quality, and process performance, particularly for challenging protein formats such as multispecific antibodies and fusion proteins.
Under the collaboration, Zylidac will initially transfer Prolific’s process to a 50-litre manufacturing scale, followed by expansion to 250 litres and subsequent GMP manufacturing activities. The partnership establishes a development-to-manufacturing pathway in which programmes can progress from Prolific’s cell line platform into Zylidac’s biologics manufacturing infrastructure.
The collaboration broadens Zylidac’s access to advanced bioprocessing technologies while strengthening its position in complex biologics manufacturing.
Zylidac Bio occupies a strategically relevant position in the U.S. biologics outsourcing market as an integrated, commercial-scale CDMO focused on complex protein therapeutics. Its establishment through Zydus Lifesciences’ acquisition of Agenus’ manufacturing assets provides an operational foundation distinct from newly constructed CDMO ventures, combining established infrastructure, experienced scientific personnel, and substantial capital investment.
Its primary differentiation is the integration of cell line development, upstream and downstream process development, drug substance manufacturing, sterile fill-finish, analytical testing, and packaging within a single California facility. This model addresses a common challenge in biologics outsourcing: the technical complexity, cost, and scheduling risk associated with transferring molecules between development laboratories, clinical manufacturing facilities, and commercial production sites.
The company’s manufacturing infrastructure, including four 2,000-litre single-use bioreactors, positions it to support programmes transitioning from clinical development into larger-scale biologics production. Its focus on monoclonal antibodies, bispecific and multispecific antibodies, fusion proteins, and biosimilars aligns with pharmaceutical and biotechnology developers seeking specialised manufacturing capabilities for increasingly complex biologic molecules.
Zylidac also benefits from its location in the San Francisco Bay Area, providing geographic proximity to biotechnology companies and developers requiring U.S.-based biologics manufacturing partners. Its ownership by Zydus Lifesciences adds the financial, operational, and pharmaceutical manufacturing backing of an established international life sciences group.
The October 2026 partnership with Prolific Machines further differentiates Zylidac through access to light-controlled biomanufacturing technology, potentially expanding its capabilities in difficult-to-express proteins and advanced biologics production. However, the partnership’s large-scale manufacturing benefits remain subject to successful technology transfer, process validation, and GMP implementation.
Within the broader CDMO competitive landscape, Zylidac is positioned to compete for biologics development and manufacturing programmes against established service providers such as Lonza, AGC Biologics, Samsung Biologics, and FUJIFILM Biotechnologies, although its current manufacturing footprint is substantially more concentrated than those of larger global competitors.